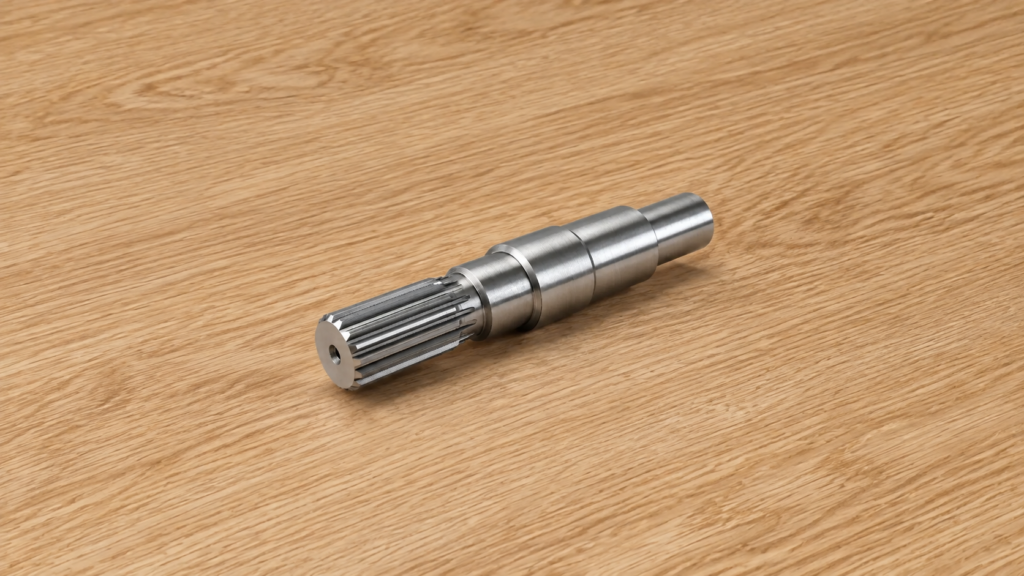
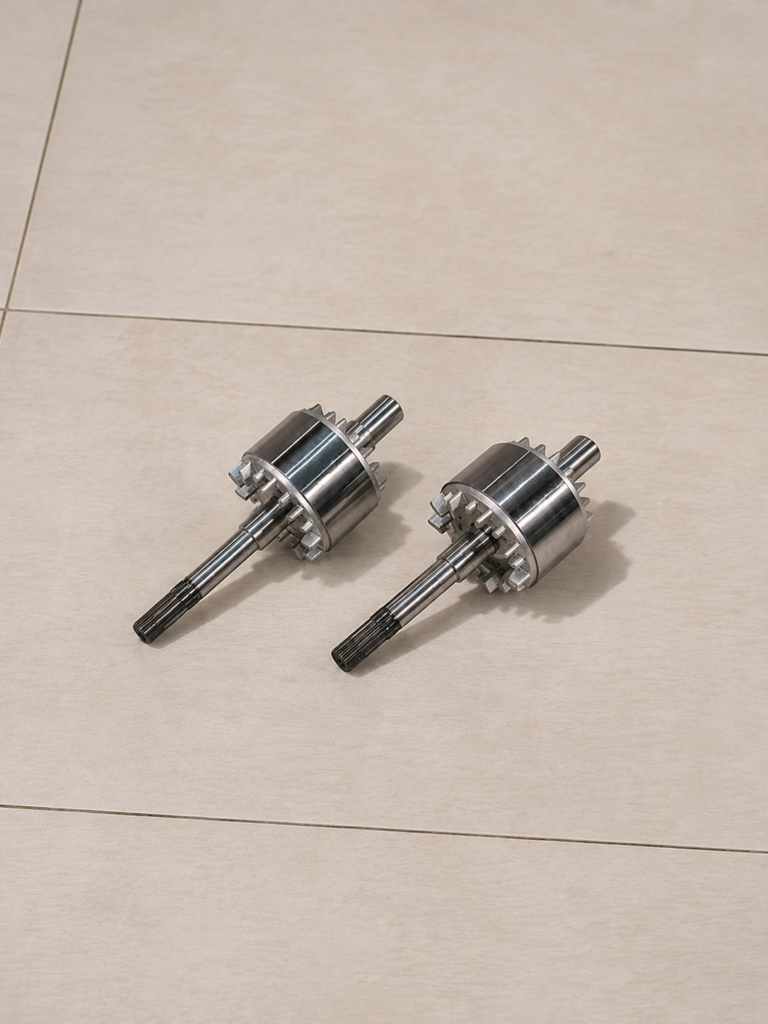
Why Is Small-Batch Consistency Difficult?
Small batch tight tolerance machining requires every part to meet the drawing requirements despite limited production quantities.
Because the process has less time to stabilize, setup errors, tool wear, material variation, temperature changes, and measurement inconsistencies can quickly affect dimensional accuracy. Effective control must therefore cover the entire manufacturing process.
1. Review Critical Features
Before production, review the drawing and identify critical dimensions, geometric tolerances, inspection datums, surface finish requirements, mating features, and dimensions affected by surface treatment.
This review determines which features require dedicated fixtures, tighter process monitoring, or additional inspection.
2. Maintain a Stable Setup
Repeatedly removing and repositioning a part can introduce alignment errors. Critical features should be machined in one setup whenever possible.
Soft jaws, locating pins, and dedicated fixtures can improve repeatability. Clamping force must remain consistent, particularly for thin-walled parts that may deform during machining.
3. Control Materials and Tooling
Material from different batches may vary in hardness, internal stress, and machinability. Using material from the same batch, together with proper material certificates and traceability records, helps reduce variation.
Tool wear is another major source of dimensional drift. Tool runout, tool life, cutting parameters, and replacement timing should be controlled. After replacing a critical finishing tool, the first part should be reverified before continuing production.
For stress-sensitive components, rough machining followed by stress relief may be required before final finishing.
4. Approve the First Part
The first completed part should be fully inspected before the remaining batch is machined. This verifies the setup, CNC program, tooling, workholding, and measurement method.
If a dimension approaches the tolerance limit, adjust the process before continuing. Positioning dimensions near the center of the tolerance range provides greater allowance for normal process variation.
5. Perform In-Process Inspection
Final inspection alone cannot prevent variation across a small batch. Critical dimensions should be checked at defined intervals using suitable equipment, such as micrometers, bore gauges, height gauges, plug or ring gauges, and coordinate measuring machines.
Parts should be measured after reaching a stable temperature. The same inspection method and measurement reference should be maintained throughout the batch.
6. Maintain Quality Records
Inspection records help identify dimensional trends and support repeat production. Depending on project requirements, records may include material batch information, first-part results, in-process measurements, final inspection data, equipment identification, and nonconformance records.
These documents also provide traceability and improve process repeatability when the same component is reordered.

Final Quality Checklist
Before releasing the batch, confirm that:
- Critical dimensions and geometric tolerances meet the drawing.
- All parts were inspected using a consistent method.
- Measuring equipment was calibrated.
- Surface treatment did not affect final dimensions.
- Parts are clean, identified, and traceable.
Conclusion
Consistent small batch tight tolerance machining requires control of the complete process rather than the CNC machine alone.
Stable workholding, controlled materials, managed tool wear, first-part approval, in-process inspection, and documented quality results work together to reduce dimensional variation.
If your components require tight tolerances, send us the drawings, material, quantity, and finishing requirements. Our team can evaluate the project and develop an appropriate machining and inspection plan.