Project Overview
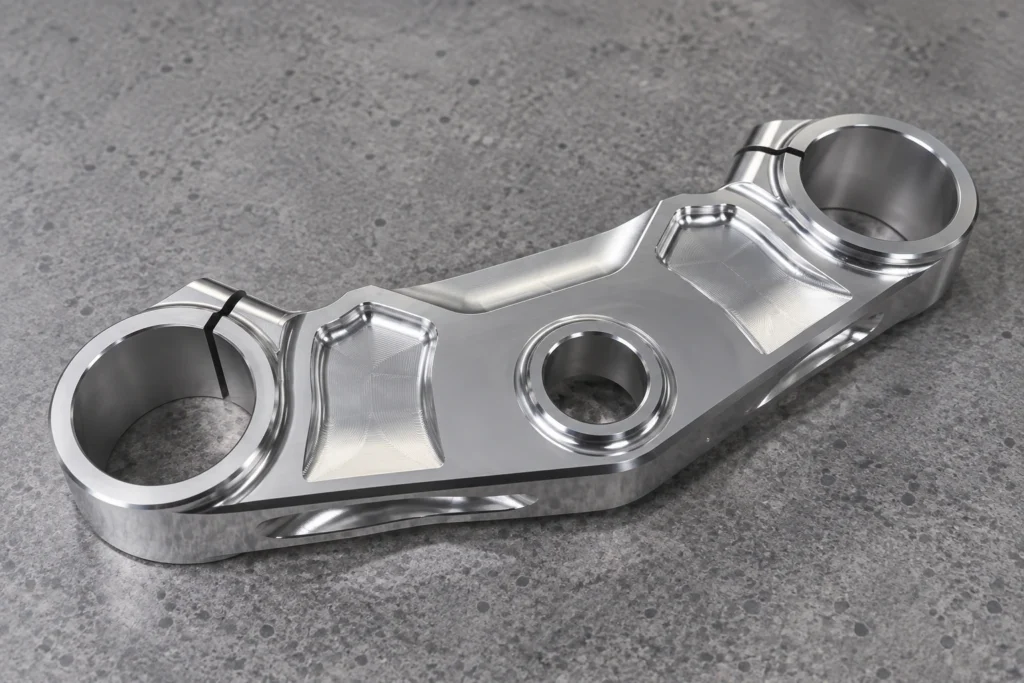
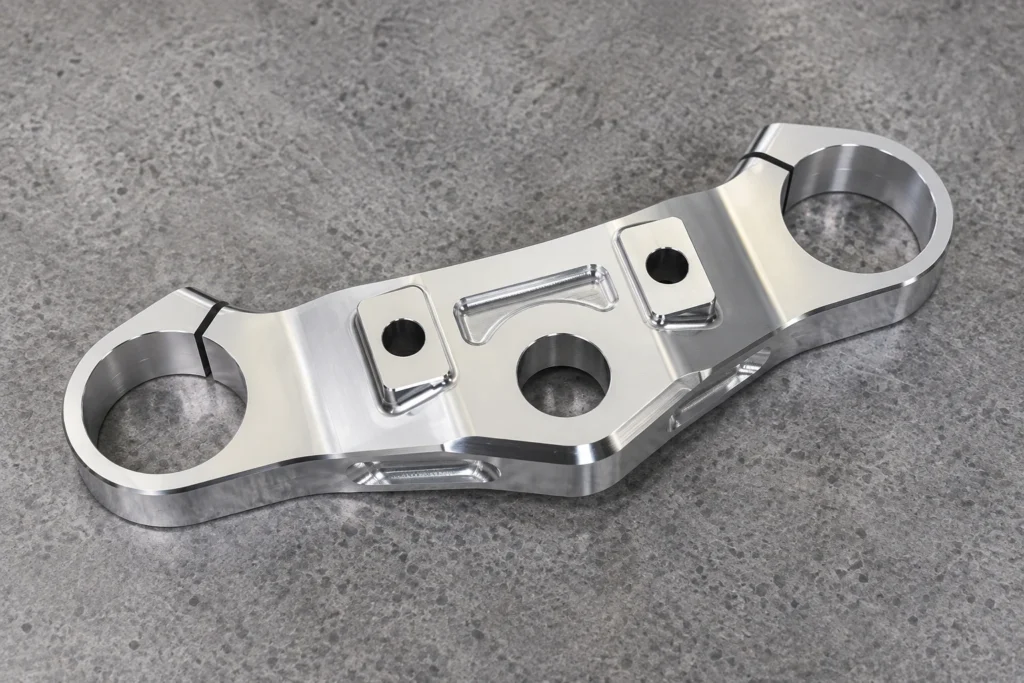
This project involved precision CNC machining of 7075 aluminum motorcycle triple clamp components for a steering assembly.
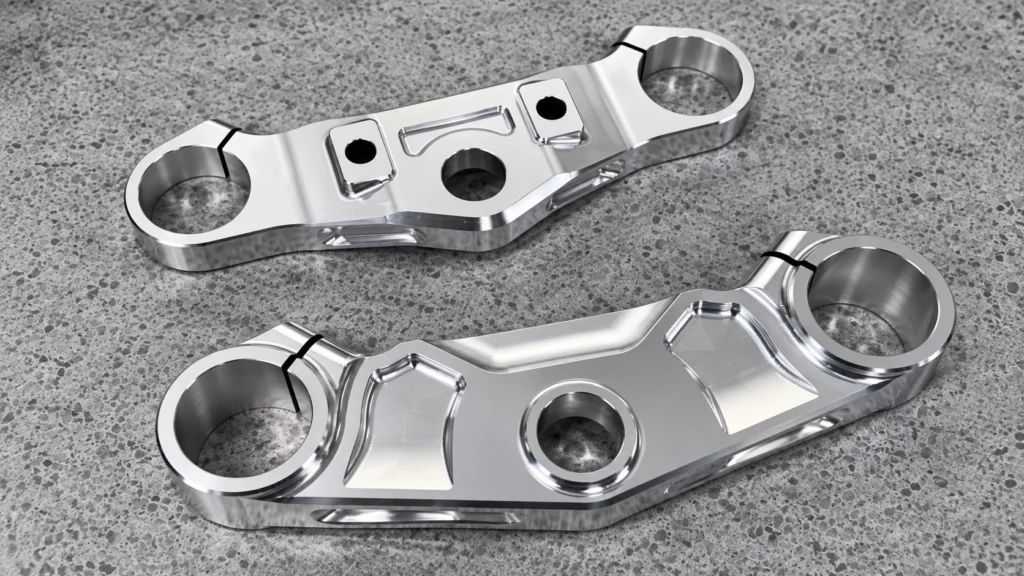
The parts feature two large fork bores, a central steering stem opening, split-clamp sections, mounting holes, and contoured surfaces. Maintaining the relationship between these features was important for proper alignment and assembly.
Machining Challenges
The main challenge was maintaining alignment between the fork bores, steering stem opening, and surrounding mounting features while controlling distortion during material removal.
Key machining considerations included:
- Accurate positioning of the two fork bores
- Alignment with the central steering stem opening
- Stable machining of split-clamp features
- Controlling distortion during material removal
- Maintaining clean visible machined surfaces
Our Solution
The machining process was planned around the primary bore locations and reference surfaces to establish stable datums before secondary features were produced.
CNC milling and precision boring were used for the fork bores, steering stem opening, mounting holes, pockets, and external profiles. Roughing and finishing operations were sequenced to maintain rigidity and preserve critical feature relationships.
- Precision boring of fork and steering stem features
- CNC milling of pockets, profiles, and mounting areas
- Controlled datum setup for feature alignment
- Optimized roughing and finishing sequence
- In-process verification of critical dimensions
Inspection & Quality Control
Inspection focused on bore diameter, bore position, steering stem alignment, clamping features, and mounting locations. Finished surfaces and edges were also visually checked before shipment.
Inspection items included:
- Fork bore dimensional inspection
- Steering stem opening verification
- Bore position and alignment checks
- Clamping and mounting feature inspection
- Visual inspection of machined surfaces
Results
The completed 7075 aluminum motorcycle triple clamp components achieved consistent geometry across the fork bores, steering stem opening, clamping sections, and machined profiles.
Careful datum control and machining sequence planning helped maintain critical bore alignment while controlling distortion during machining.
The finished parts showed clean contoured surfaces, well-defined mounting features, and consistent geometry suitable for final assembly.