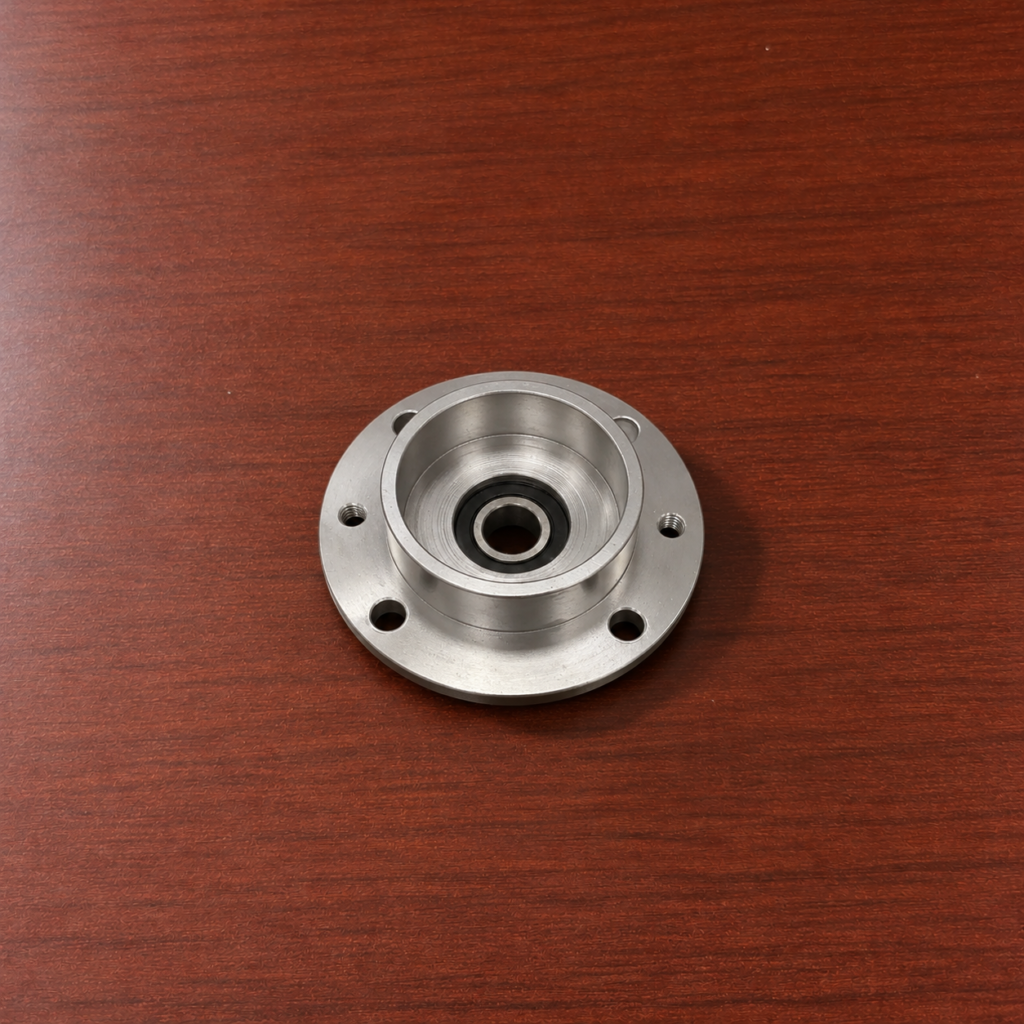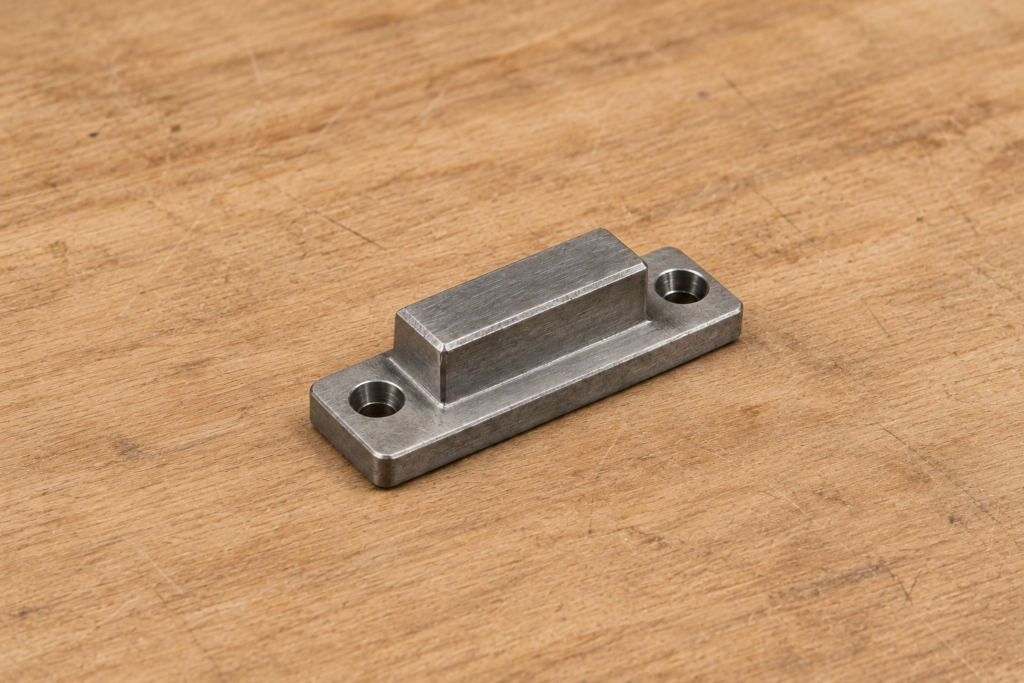
Pneumatic gripper connection plate CNC machining creates the interface between a gripper body and a robot, slide unit or handling fixture. The plate commonly includes mounting holes, locating bores, adjustment slots and recessed areas within a compact rectangular profile.
Because each connected component uses a different hole pattern, the plate must transfer their positions through one consistent coordinate system.
Create the Primary Reference Face
The blank is clamped with enough support beneath the future mounting areas. Face milling removes surface variation and establishes the first reference plane.
One long edge and one adjacent end are then machined to create the X- and Y-axis references. These surfaces allow every slot and hole to be positioned from the same corner.
The plate is kept relatively solid during this stage. Removing large internal openings too early can reduce support and allow the workpiece to move during hole machining.
Open the Main Slots
Connection plates may use straight slots for adjustment, clearance slots for moving jaws or wider openings for pneumatic lines.
An end mill enters through a predrilled point or follows a ramping path into the material. Rough passes remove the central stock while leaving a small allowance on the slot walls.
The finishing pass follows the complete slot profile to produce consistent width and smooth end radii. When several parallel slots are required, they are machined from the same coordinate reference rather than positioned from one another.
Produce the Mounting Pattern
Gripper bodies commonly use threaded holes combined with locating pins. The robot-side pattern may instead require clearance holes, counterbores or countersinks.
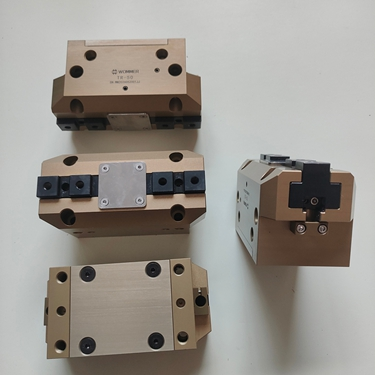
Each hole type follows a separate operation:
| Plate feature | Machining operation |
|---|---|
| Locating hole | Drill and ream |
| Threaded mounting hole | Drill and tap |
| Bolt clearance hole | Drill or circular mill |
| Recessed screw seat | Counterbore or countersink |
Locating holes are completed before less critical clearance features. This allows the gripper position to be established by the pins rather than by movement inside the bolt holes.
Connect Features from the Second Side
Some plates contain rear pockets for bolt heads, pneumatic fittings or cable clearance. The workpiece is reversed and located from the finished edges or dowel holes.
The second face is milled to final thickness before the rear pockets are opened. Hole positions are transferred from the established datum system so counterbores remain concentric with the through holes produced in the first setup.
A shallow step may also be machined around the mounting area to fit a corresponding recess on the gripper body.
Complete the Plate Profile
The outside contour is finished after the internal features have been completed. Tabs or an uncut boundary can retain the part until the final profiling pass.
Edges around slots and holes are deburred without changing the locating surfaces. Pneumatic gripper connection plate CNC machining is complete when the gripper-side and robot-side patterns remain aligned through the shared plate coordinates.