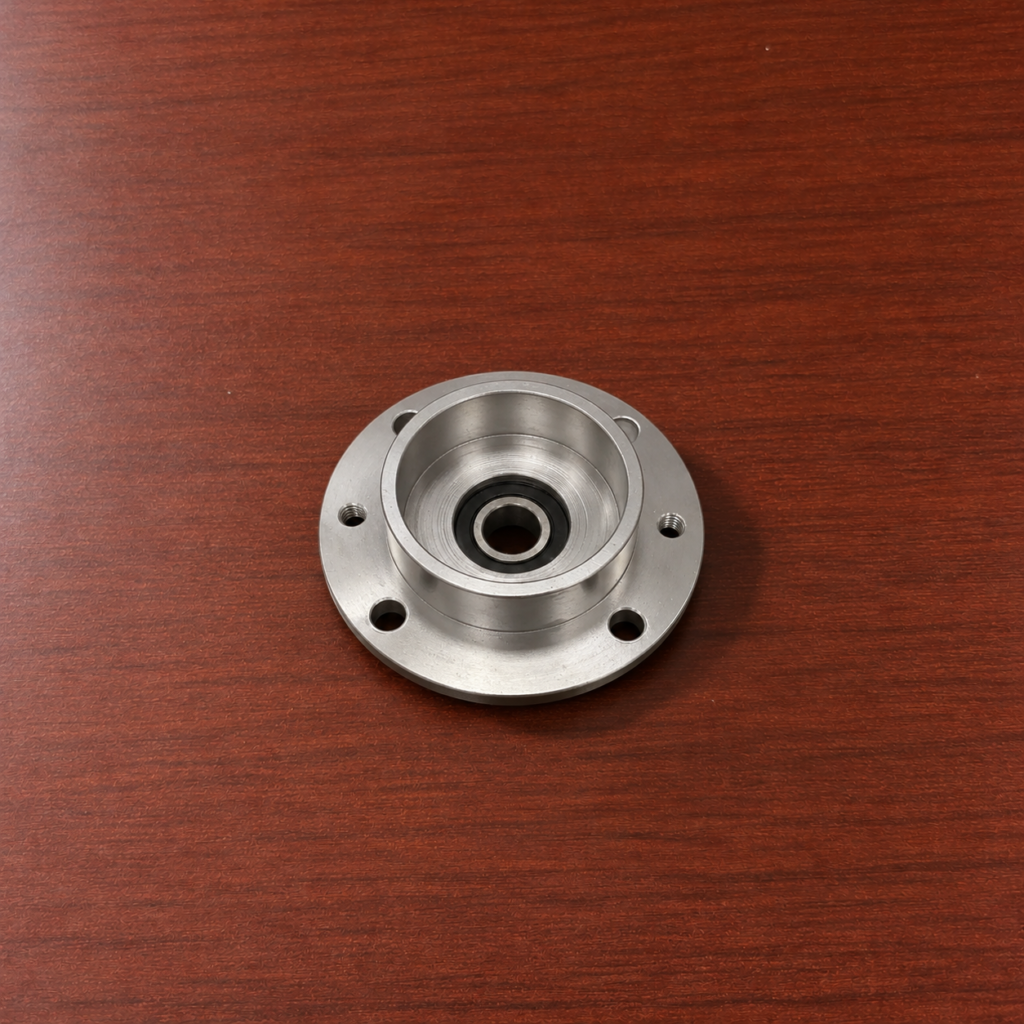
Linear module slide CNC machining creates the moving platform that supports tooling, sensors or automation fixtures. Its most important features are usually not the visible outer edges but the surfaces and holes used to mount the linear guide blocks.
These features form a connected locating system. The rail seat controls height, the shoulder controls lateral position, and the mounting holes secure the assembled components.
Begin with the Underside Datum
The blank is first supported on a stable fixture so its underside can be faced. This surface becomes the primary reference for the remaining operations.
Material is removed in balanced passes rather than from one small area at a time. For a wide or relatively thin slide, uneven cutting may release internal stress and cause the plate to move after unclamping.
Once the underside is complete, the component is reversed and located from the machined datum. The upper face can then be brought to final thickness.
Cut the Rail Seats Together
A slide may carry two guide blocks or two parallel rail-contact areas. Both seats should be machined within the same setup whenever possible.
Rough milling removes the main stock from each recessed area. The finishing tool then travels across the mounting surfaces using the same coordinate reference. This approach keeps the two seats at a consistent height.
A light final pass completes the contact areas without repeatedly entering and leaving the surface. Sharp chips must be cleared before finishing because trapped debris can mark the rail seat.
Use the Shoulder as a Positioning Feature
Mounting screws hold the guide blocks down, but they do not always define their lateral position. A machined shoulder or side face provides a more repeatable locating edge.
The shoulder is finished in relation to the rail seat so both features meet at the intended corner. Tool reach must be considered here: an oversized cutter may leave material near the intersection, preventing the guide block from sitting fully against the reference.
A smaller end mill can clean the corner or create the specified relief before hole machining begins.
Transfer the Datum to the Hole Pattern
The mounting holes are programmed from the same origin used for the rail seats. This prevents the hole pattern from shifting independently of the locating surfaces.

Spot drilling establishes each position before drilling. Depending on the assembly design, the holes may then receive:
- threads for directly fastening the guide blocks;
- counterbores for recessed screw heads;
- dowel holes for repeated positioning;
- through-holes for fastening from the opposite side.
Dowel holes are normally drilled undersize and finished by reaming. Threaded holes require enough chip clearance at the bottom if they are blind.
Complete the Remaining Faces
After the guide-rail interface is established, the slide can be repositioned for side holes, end mounting holes or sensor-bracket features. Finished faces and locating holes provide references for these secondary setups.
Long side holes should be drilled with the component supported close to the cutting area. This limits vibration and prevents the slide from lifting away from the fixture.
Burrs around mounting holes and rail-seat edges are removed carefully so they cannot hold the guide blocks above the finished surface. Effective linear module slide CNC machining keeps the mounting face, locating shoulder and hole pattern tied to one consistent datum system.