CNC Machining Internal Corners & Radii Guidelines
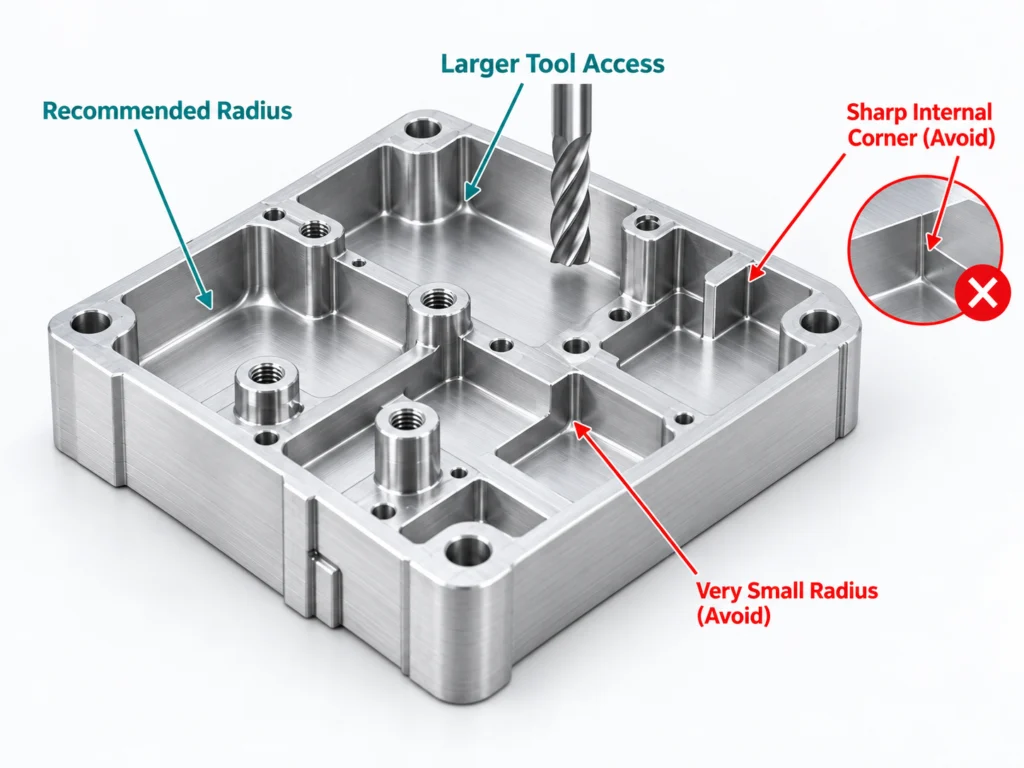
Design internal corners with appropriate radii to improve tool access, reduce machining time, and avoid unnecessary small-diameter cutters.
Get a Quote
CNC machining internal corners and radii showing recommended radius and tool access
INTERNAL CORNER RADIUS BASICS

Design Internal Corners for Easier CNC Machining

Larger internal radii allow the use of larger, more rigid cutters, improve tool access, and help reduce machining time, chatter, and cost.
Feature
Recommended
Avoid
Notes
Internal Corners
Use the largest practical radius
Sharp 90° internal corners
CNC end mills naturally create rounded internal corners
Pocket Corners
Add generous corner radii
Very small corner radii
Larger radii allow larger, more rigid cutting tools
Deep Pockets
Increase radius as depth increases
Small radius in deep cavities
Deep features require longer tools and greater rigidity
Bottom Corners
Add an appropriate bottom corner radius
Sharp internal bottom corners
Improves tool access and reduces cutter loading.
Square Mating Features
Use reliefs or dog-bone corners if required
Unrelieved sharp internal corners
Relief features can provide clearance for mating parts
Tool Access
Keep corners accessible to standard cutters
Restricted tool access in narrow corners
Better access reduces special tooling and extra setups
Design Tip: Use the largest internal radius your design allows. Larger radii generally improve machining stability and reduce machining time.
INTERNAL CORNER MACHINING

Internal Corner Machining Considerations
Tool Diameter
Larger corner radii allow the use of larger, more rigid cutters.
Tool Reach
Deep pockets require longer tools, which can increase deflection and vibration.
Corner Radius
Very small internal radii may require smaller cutters, increasing machining time and tool deflection.
Pocket Depth
Deeper cavities usually benefit from larger internal corner radii.
Tool Access
Restricted corners or narrow pockets can require special tooling or additional setups.
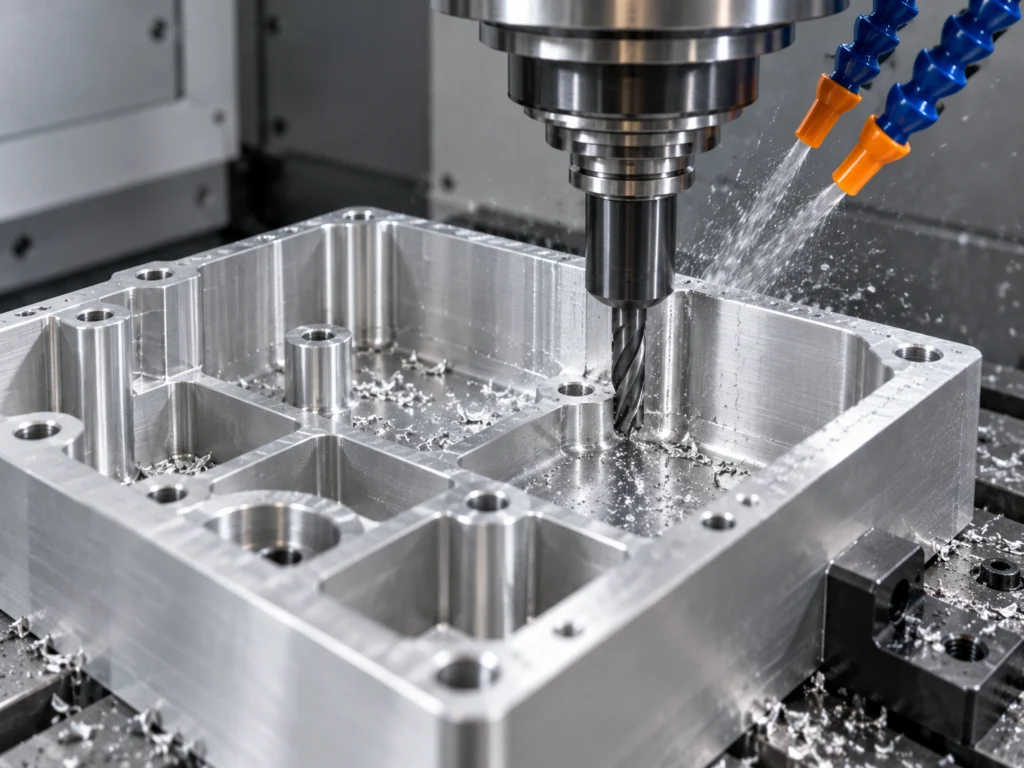
CNC milling internal corners and pocket radii in an aluminum part
DESIGN EXAMPLES

Good vs. Poor Internal Corner Design

Compare recommended and poor internal corner designs for more efficient and reliable CNC machining.
Recommended vs sharp internal corner design for CNC machining

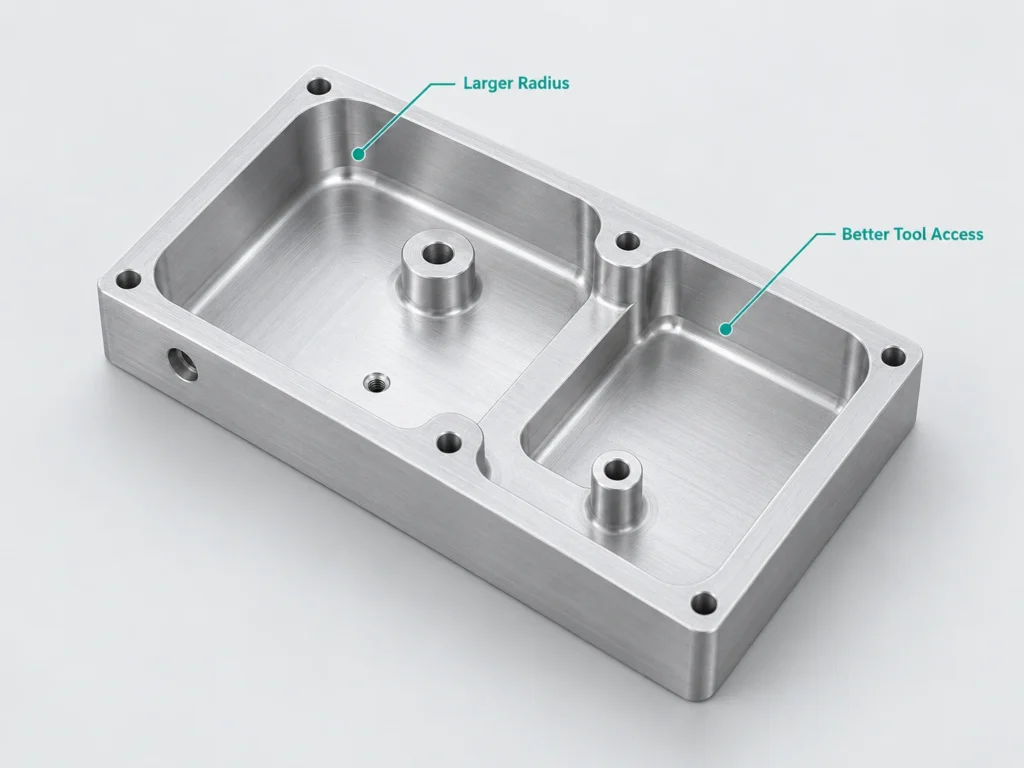
Larger Internal Radius

Use the largest practical internal radius to allow larger, more rigid cutting tools.
Internal corner radius design for deep CNC machined pockets

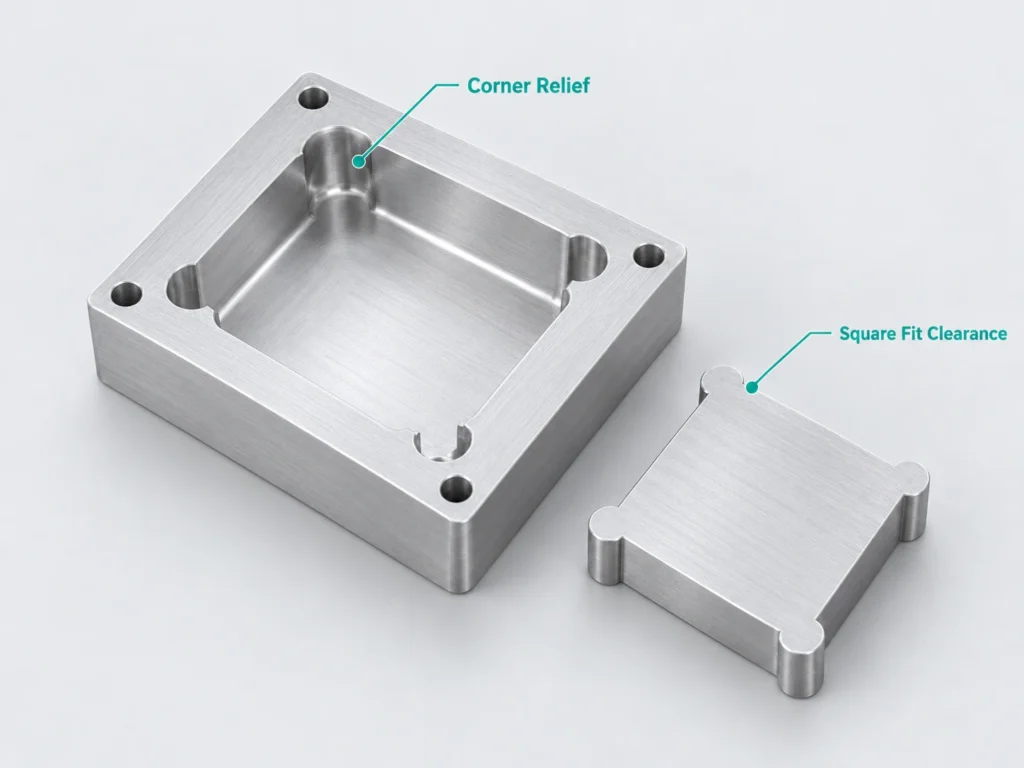
Corner Relief for Square Fits

Add corner reliefs or dog-bone features when a square mating part needs full clearance.
Dog-bone corner relief for square mating parts in CNC machining

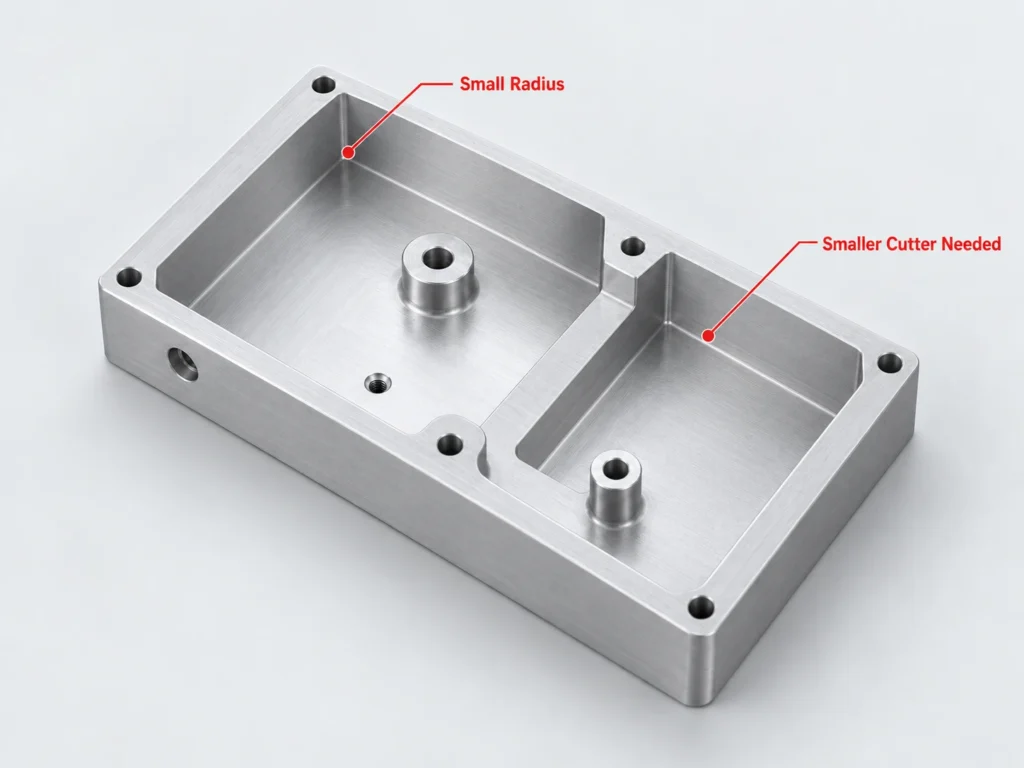
Very Small Internal Radius

Small internal radii require smaller cutters, increasing machining time and tool deflection.
CNC tool access for internal corners and narrow pockets

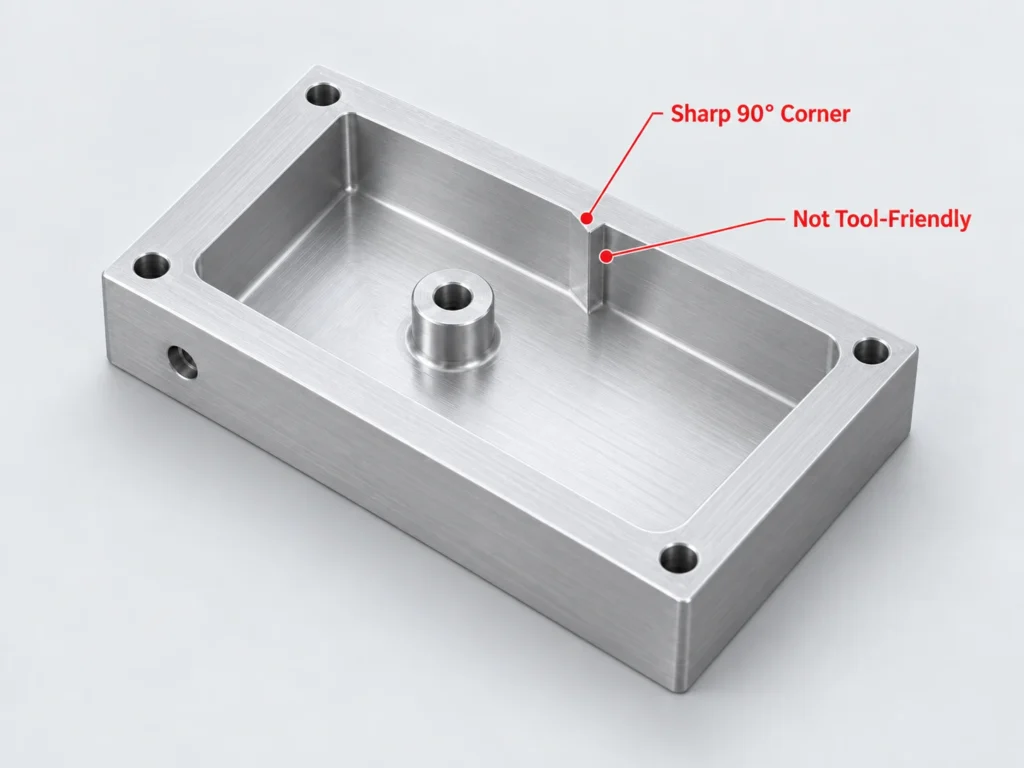
Sharp 90° Internal Corner

Avoid specifying sharp internal corners that standard end mills cannot produce directly.

Need an Internal Corner Design Review?

Send us your drawings or CAD files. We can review internal radii, pocket depth, tool access, corner reliefs, and manufacturability before production.
FAQ

Internal Corners & Radii FAQs

Common questions about internal corner radii and CNC machining design.

CNC end mills are round, so they naturally leave a radius in internal corners. Adding an appropriate radius improves tool access, allows the use of larger and more rigid cutters, and helps reduce machining time and tool wear.

Use the largest practical internal radius your design allows. Larger radii generally allow larger, more rigid cutters and improve machining stability. The final radius should be selected based on pocket depth, tool diameter, part geometry, and functional requirements.

Generally, yes. Deep pockets require longer cutting tools, which are more prone to deflection and vibration. Increasing the internal corner radius allows the use of a larger and more rigid tool.

Standard CNC milling cannot directly produce a perfectly sharp 90° internal corner because end mills have a finite radius. If a sharp fit is required, corner reliefs, dog-bone features, EDM, or another secondary process may be considered.

Dog-bone corners are small relief features added to internal corners to provide clearance for square mating parts. They are commonly used when a rectangular insert or component needs to fit fully into a CNC-milled pocket.